Mastering Waterjet Cutting Pressure: A Complete Guide
When you hear the term waterjet cutting machine pressure, you might picture a massive hose blasting material into oblivion. In reality, the pressure is the delicate balance that determines cut quality, speed, and even the lifespan of the nozzle. Whether you’re a hobbyist tinkering in a small workshop or a production manager overseeing a high‑volume line, grasping how pressure works is essential for getting the most out of a waterjet system.
Understanding Waterjet Cutting Machine Pressure
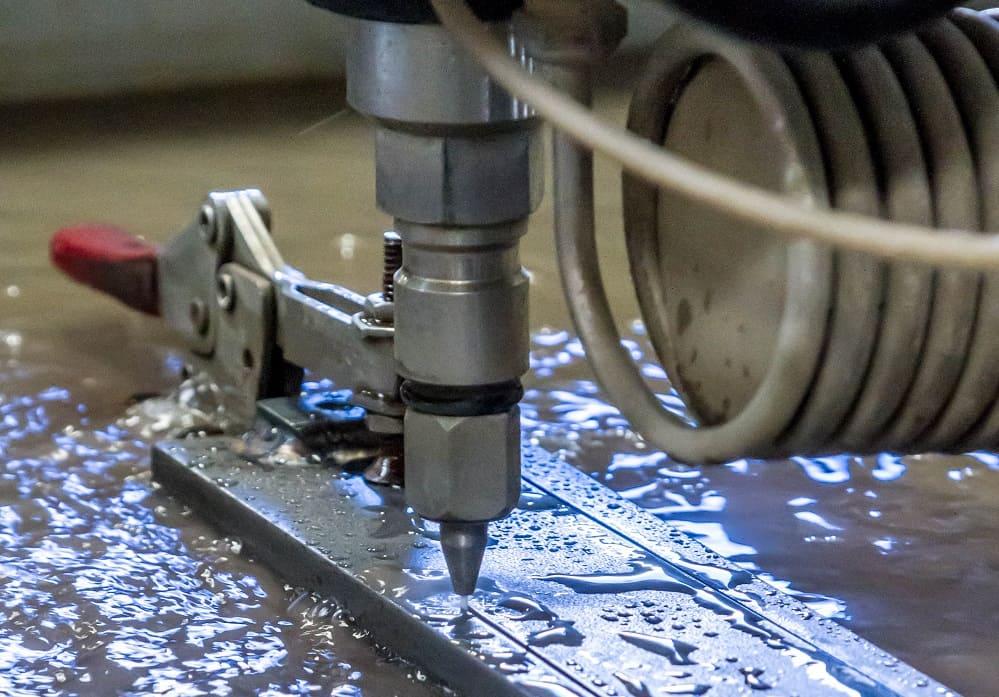
At its core, a waterjet cutter uses a pump to accelerate water to extreme velocities—often exceeding 2,000 feet per second. This kinetic energy, measured in pounds per square inch (psi), is what slices through metal, stone, or composite materials. The higher the psi, the more energy is delivered to the cutting point, allowing the jet to penetrate tougher substrates.
But “higher is better” is an oversimplification. Too much pressure can erode the abrasive, wear out the focusing lens, or create excessive taper in the cut. Too little, and the jet stalls, producing ragged edges or missing the material entirely. The sweet spot varies by material, thickness, and desired finish.
Typical Pressure Ranges and What They Mean
Most industrial waterjet machines operate between 30,000 and 60,000 psi. Here’s a quick snapshot of what those numbers translate to in practice:
- 30,000 psi – Suitable for soft metals (aluminum, copper), plastics, and thin sheets up to ¼ inch.
- 45,000 psi – The workhorse range for medium‑hard steels, glass, and stone up to ½ inch.
- 60,000 psi – Reserved for thick, hard materials like titanium, aerospace alloys, or dense ceramics.
Some ultra‑high‑pressure (UHP) systems push beyond 90,000 psi, but those are niche installations with specialized nozzles and safety protocols.
Factors That Influence Required Pressure
Several variables dictate the pressure you’ll need for a given job:
- Material hardness – Harder alloys demand more force to break molecular bonds.
- Thickness – As thickness increases, the jet must maintain momentum longer, calling for higher psi.
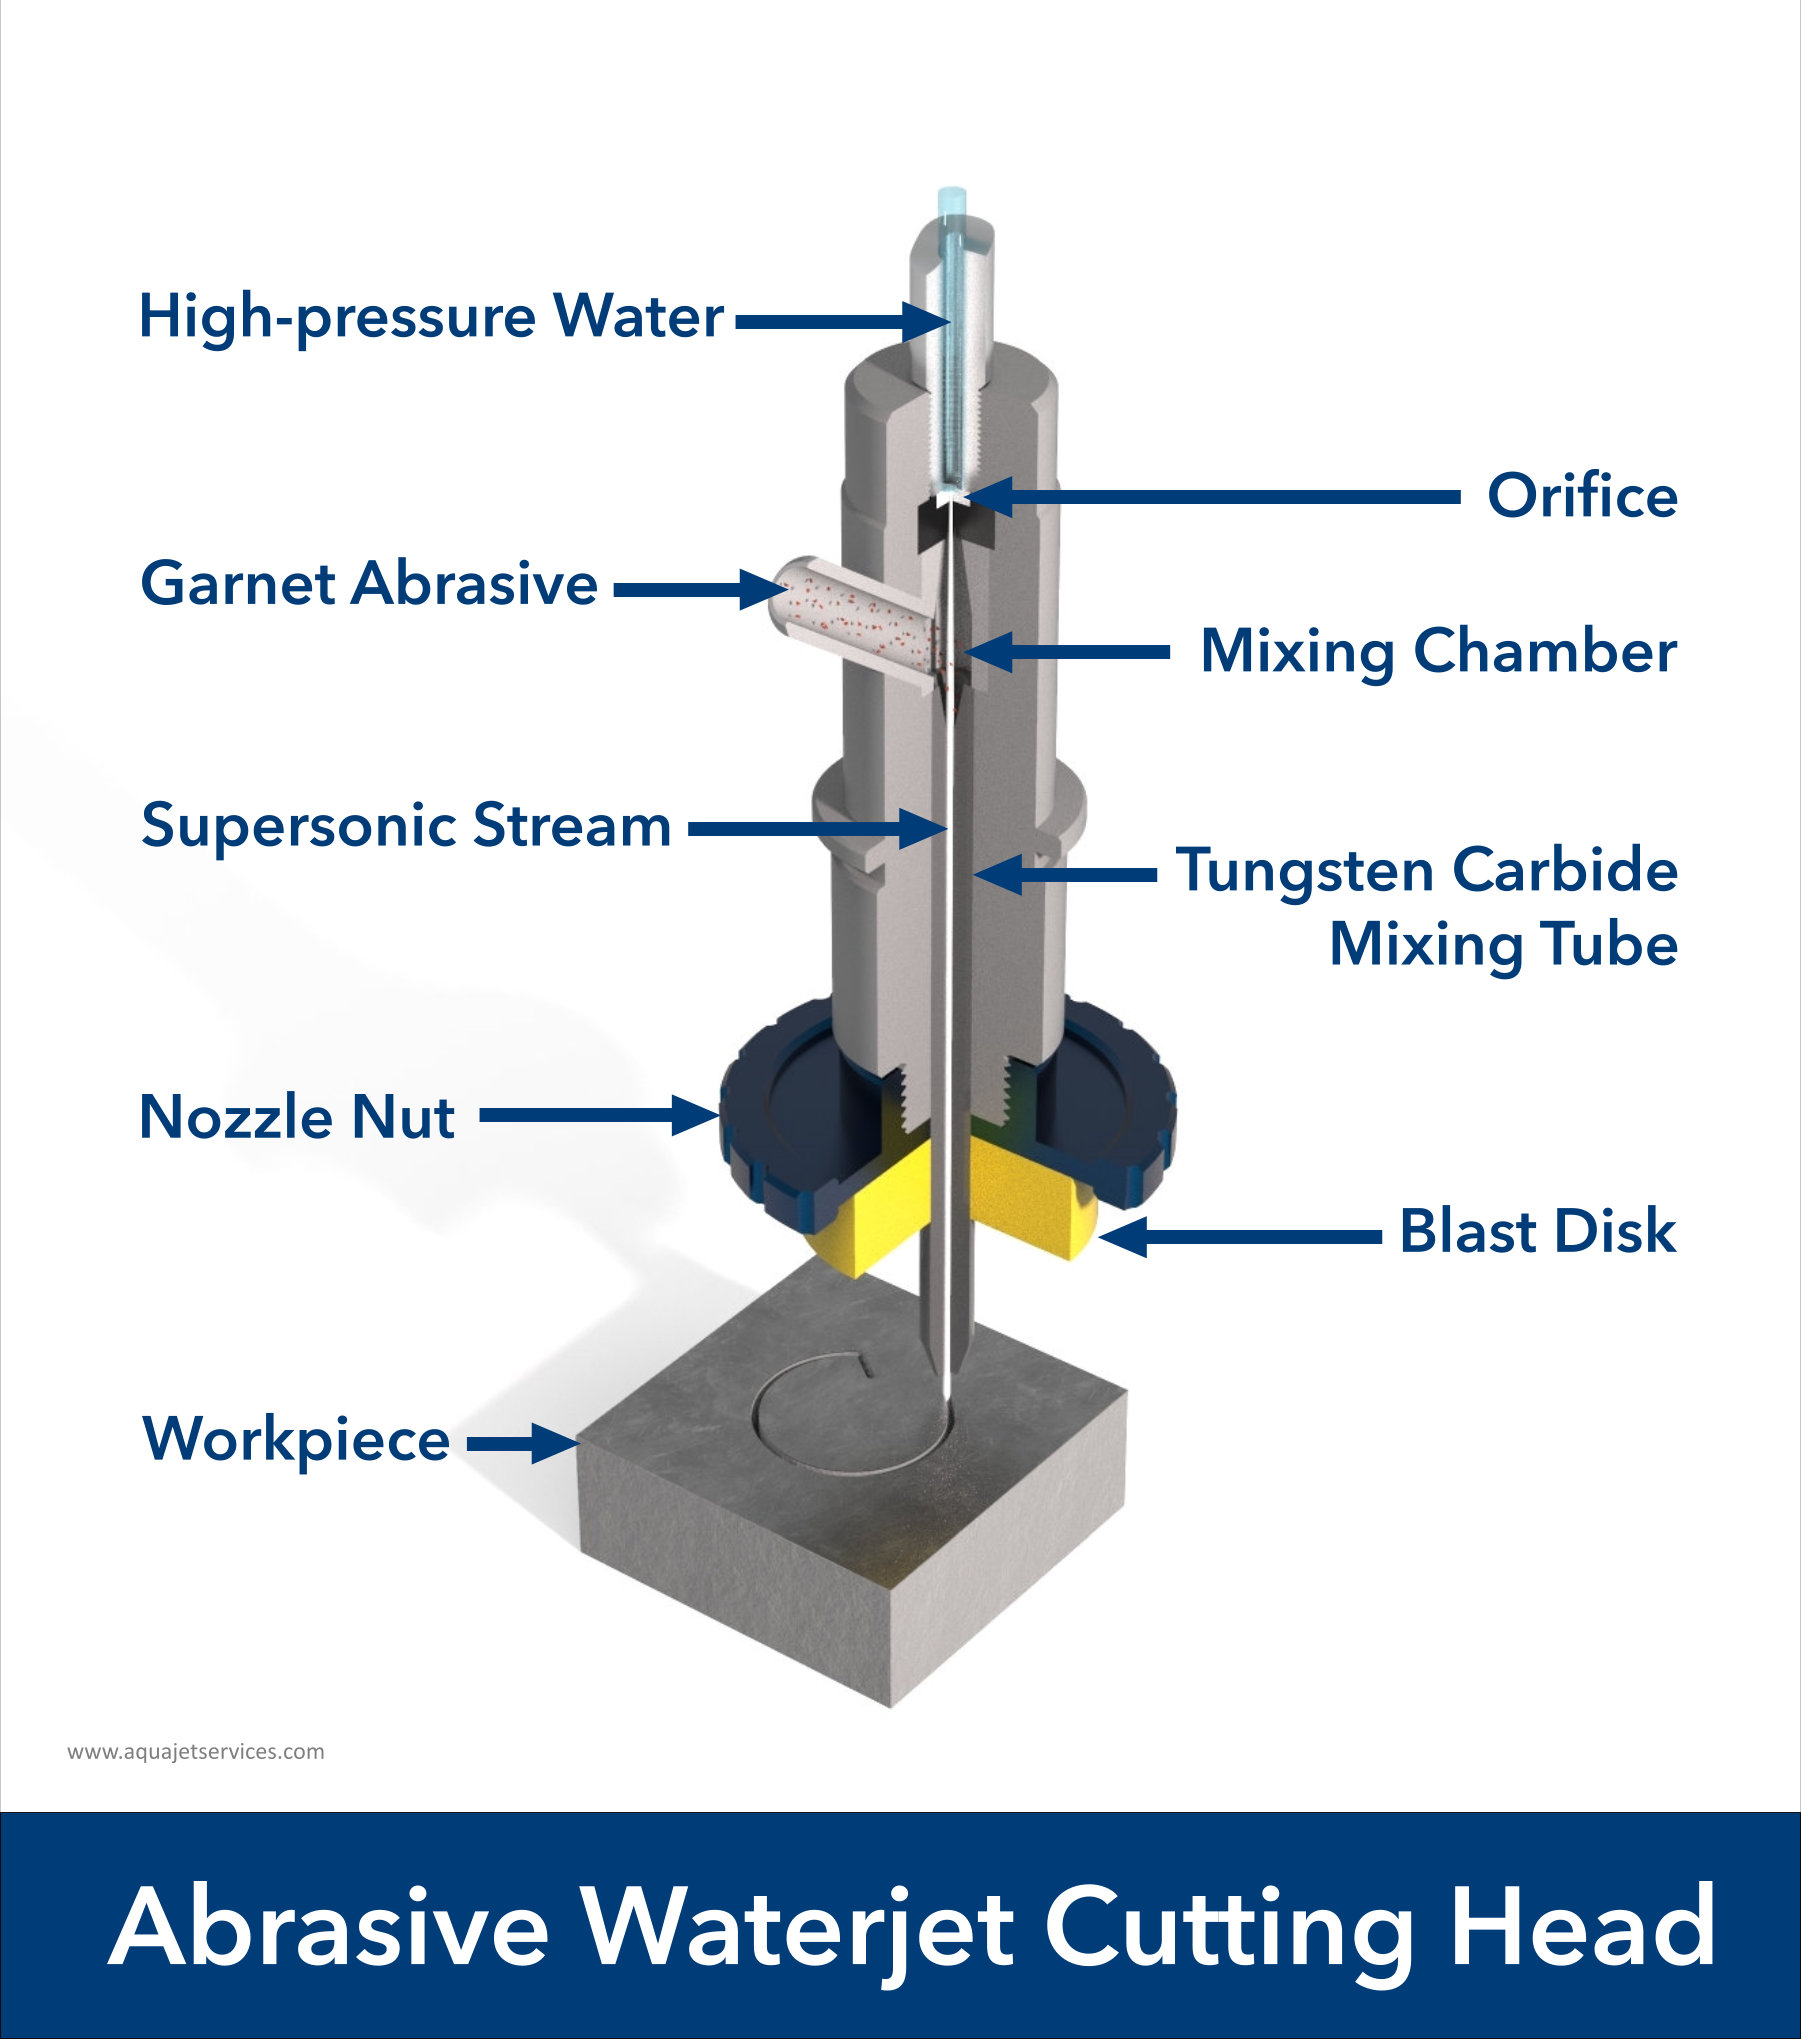
- Abrasive type and concentration – Garnet is common, but the particle size and loading affect how much pressure is needed to carry the abrasive through the cut.
- Nozzle diameter – Smaller orifices focus the jet, often allowing lower pressure to achieve the same cut depth.
- Cutting speed – Faster cuts require more pressure to keep the jet from dissipating.
Balancing these elements is part art, part engineering. A seasoned operator will tweak one knob at a time, watching how the kerf responds.
Choosing the Right Pressure for Your Material
Start with the manufacturer’s baseline recommendations—most suppliers publish charts linking material type, thickness, and pressure. From there, follow a systematic approach:
- Set a baseline based on the chart (e.g., 45,000 psi for ¼‑inch stainless steel).
- Run a test cut on a scrap piece, noting kerf width, edge quality, and any taper.
- Adjust incrementally—increase pressure by 2,000–3,000 psi if the cut is incomplete, or lower it if you see excessive wear on the nozzle.
- Document the settings for repeatability, especially if you move from prototype to production.
Remember that pressure isn’t the only lever. You can also play with traverse speed, stand‑off distance, and abrasive flow rate to fine‑tune the outcome.
Maintaining Pressure Consistency
Even the best‑designed pump can suffer pressure dips if the system isn’t cared for. Regular maintenance tasks include:
- Inspecting seals and O‑rings for wear—leaks are the silent killers of pressure stability.
- Flushing the high‑pressure line after each job to prevent abrasive buildup.
- Monitoring pump temperature; overheating can cause pressure fluctuations.
- Calibrating pressure gauges at least quarterly to ensure read‑outs match actual output.
A consistent pressure profile not only improves cut quality but also extends the life of costly components like the high‑pressure pump and focusing lens.
Safety Considerations with High‑Pressure Waterjets
Water at 60,000 psi is more dangerous than a loaded gun. Safety isn’t an afterthought; it’s built into the system design:
- Enclosed work chambers with interlocks prevent accidental exposure.
- Pressure relief valves that vent excess energy in a controlled manner.
- PPE—cut‑resistant gloves, safety glasses, and ear protection are mandatory.
- Training—operators should be certified, familiar with emergency shut‑down procedures, and aware of the hazards of high‑velocity water and abrasive particles.
Never bypass safety devices to gain a “speed advantage.” The cost of an injury far outweighs any productivity gain.
Frequently Asked Questions
What is the minimum pressure needed to cut steel?
For mild steel up to ¼ inch thick, most machines can achieve a clean cut at around 30,000–35,000 psi, provided the abrasive flow is optimized.
Can I use a waterjet to cut wood without abrasive?
Yes, pure water can slice thin plywood or MDF at pressures above 40,000 psi, but the edge will be rougher compared to an abrasive‑assisted cut.
How often should I replace the focusing lens?
Lens life varies with pressure and abrasive load, but a typical interval is 1,000–1,500 hours of operation or when you notice a drop in cut precision.
Does higher pressure increase water consumption?
Higher pressure does require more power, but water usage remains relatively constant; the main variable is the amount of abrasive mixed in.