Hot vs Cold Chamber Die Casting: Which Process Yields Superior Quality?
Die casting has long been the backbone of high-volume metal production, but the debate over hot versus cold chamber techniques continues to spark interest. Both methods share the same goal—inject molten metal into a precisely machined cavity—but they differ in temperature handling, material compatibility, and performance outcomes. In this article we break down the key distinctions, compare strengths, and help you decide which method is best for your next project.
Hot vs Cold Chamber Die Casting: Key Differences
Process Overview
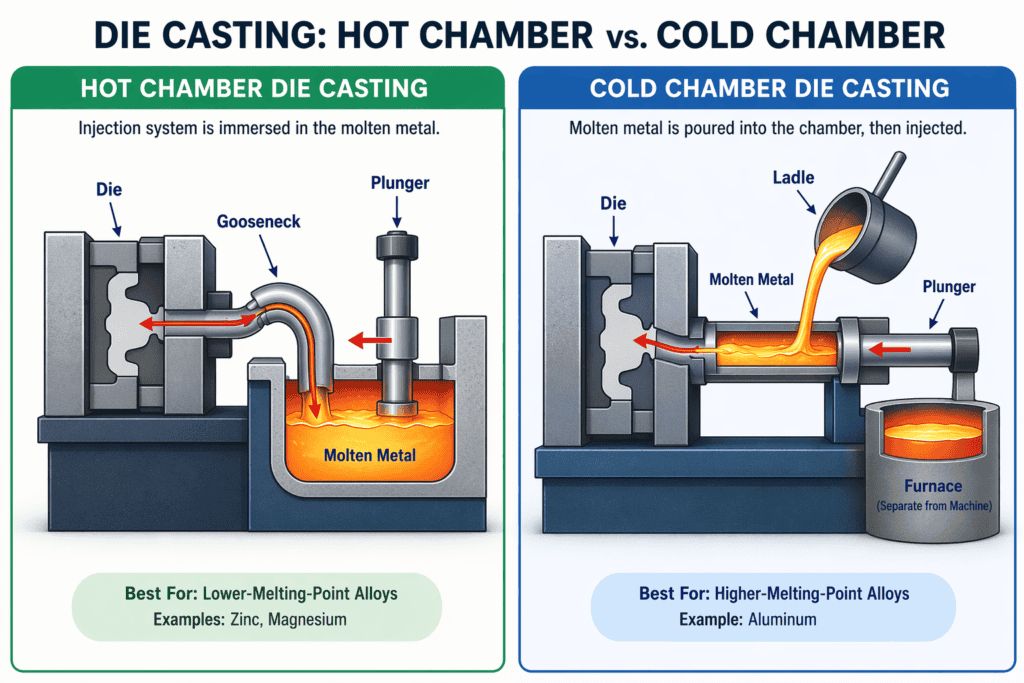
Cold chamber die casting keeps the die at a near‑ambient temperature. Molten metal is poured from a crucible into a separate injection system that delivers it under pressure into the die cavity. In contrast, hot chamber die casting integrates the melt directly inside the die itself. A small heating element melts the metal as it’s being injected, keeping the die hot and the metal liquid at a steady temperature.
Temperature Control and Material Compatibility
- Cold chamber excels with alloys that can tolerate temperature swings, such as aluminum, zinc, and magnesium. The cooler die reduces the risk of warping and thermal shock.
- Hot chamber is ideal for metals that require a uniform melt temperature—nickel, bronze, and some specialty alloys—since the die temperature is maintained throughout the cycle.
Production Speed and Throughput
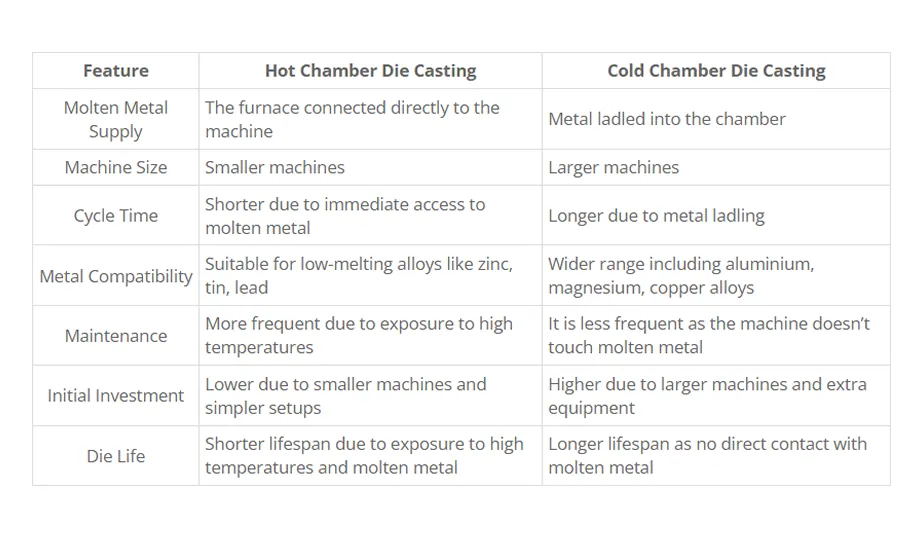
Cold chamber systems can operate at higher cycle times because the die cools more rapidly, allowing for faster demolding and reduced heating energy. Hot chamber units, however, eliminate the need for a separate melt vessel, often shortening the overall cycle. The trade‑off is that each cycle requires careful temperature monitoring to prevent overheating of the die.
Material Suitability: When One Wins Over the Other
Aluminum Alloys
Aluminum’s low melting point (around 660 °C) and good fluidity make it a natural fit for cold chamber casting. The cooler die also helps suppress porosity and promotes better surface finish.
Nickel and Bronze
These higher‑melting alloys (nickel ~1450 °C, bronze ~900 °C) benefit from hot chamber technology. The heated die keeps the metal at a stable temperature, reducing the likelihood of hot tearing and ensuring uniform grain structure.
Composite and High‑Strength Materials
When dealing with composites or alloys that have stringent thermal profiles, hot chamber die casting offers tighter temperature control. Cold chamber can still be used if the material tolerates rapid cooling and the process is optimized for minimal shrinkage.
Cost Implications and Tooling Considerations
- Die Life – Hot chamber dies typically suffer faster wear due to continuous exposure to high temperatures, but advances in thermal barrier coatings are extending longevity.
- Energy Consumption – Cold chamber processes consume more energy for melting metal in a separate furnace, while hot chamber relies on sustained heating of the die.
- Setup Times – Cold chamber setups are faster; hot chamber demands meticulous temperature calibration before each run.
- Tooling Cost – Cold chamber dies can be simpler and cheaper to manufacture, whereas hot chamber dies often require specialized alloys or coatings.
Quality Outcomes: Surface Finish, Dimensional Accuracy, and Defects
Both processes can achieve high dimensional tolerance, but the approach to defects differs.
- Porosity – Cold chamber tends to produce lower porosity because the die’s cooler surface helps trap gases. Hot chamber can exhibit higher porosity if temperature control is inadequate.
- Shrinkage – Cold chamber’s rapid cooling can cause slight shrinkage, requiring careful design compensation. Hot chamber’s steady temperature reduces shrinkage but can lead to uneven cooling if not managed.
- Hot Tearing – Rare in cold chamber but possible in hot chamber if the metal cools too quickly once it exits the die.
Surface roughness is usually smoother in cold chamber parts due to the cooler die’s ability to promote better metal flow. However, hot chamber can produce a fine finish if the melt is precisely controlled.
Common Use Cases in Industry
- Automotive – Cold chamber dominates for high‑volume components like engine blocks and housings.
- Aerospace – Hot chamber is favored for critical structural parts requiring superior metallurgical properties.
- Consumer Goods – Both processes are used, with the choice driven by material, volume, and cost constraints.
Decision‑Making Checklist
- Is the alloy low‑melting and tolerant to temperature swings? → Cold chamber.
- Does the metal need a uniform, high temperature for optimal flow? → Hot chamber.
- Is production volume extremely high and cost a primary factor? → Cold chamber.
- Is part quality and metallurgical performance the top priority? → Hot chamber.
- What is your die life expectation? Cold chamber generally outlasts hot chamber.
Frequently Asked Questions
Q1: Can I use the same die for both hot and cold chamber casting?
A1: In most cases, a die is designed specifically for one method. Switching between them requires modifications to temperature control